How to Find the Best Metal Stamping Parts in China?
Finding reliable Metal Stamping Parts in China requires more than comparing prices on a supplier website. The right partner must understand your material, drawing tolerances, production volume, and delivery expectations. Steel thickness, burr limits, hole accuracy, and surface finish can affect both performance and total cost. A professional supplier should explain these details clearly before quoting. They should also recommend suitable presses, dies, and inspection methods for your application. Ask for relevant samples, manufacturing photos, and quality records. Details matter.
A careful evaluation should include factory capability, engineering support, tooling experience, and communication speed. Look for evidence such as ISO certification, documented inspection procedures, and traceable material certificates. These documents help, but they do not prove everything. A factory visit, video audit, or independent inspection can reveal practical conditions, including machine maintenance and packing quality. Request a prototype or small trial order before approving full production. Test the parts under real operating conditions. That step may expose weaknesses early.
Price deserves attention, but the lowest quotation is rarely the safest choice. Tooling fees, material substitutions, rework, freight, and delayed shipments can change the final cost. A written agreement should define tolerances, acceptable defects, packaging, payment stages, and corrective action. No checklist is perfect. Even experienced buyers can overlook communication gaps or unclear drawings. Review the supplier’s questions carefully; thoughtful questions often show genuine technical understanding. With evidence, testing, and realistic expectations, you can select Metal Stamping Parts that remain consistent from the first batch to long-term production.
Define Your Metal Stamping Part Requirements
Finding suitable metal stamping parts in China starts with a precise requirement sheet. A clear drawing helps, but it rarely answers every production question. Specify the material grade, thickness, part dimensions, tolerances, and expected annual volume. Include the working environment, such as moisture, heat, vibration, or contact with other metals.
Small details matter. State the required surface finish, coating, edge condition, and acceptable burr height. If the part includes holes, bends, or deep draws, identify their critical measurements. A tolerance of ±0.05 mm may require different tooling from ±0.20 mm. Confirm whether the tolerance applies before or after surface treatment. This point is often missed.
Experienced engineers also define inspection requirements before requesting quotations. Ask for dimensional reports, material certificates, sample approval, and packaging details. Clarify who owns the tooling and how future maintenance will be handled. A supplier should explain the press capacity, die structure, production steps, and quality checkpoints in practical terms.
Leave room for testing. Initial prototypes may reveal springback, distortion, or unexpected scratches. That is useful feedback. A specification can be technically correct yet difficult to manufacture efficiently. Review it with a stamping engineer and revise unclear areas before mass production. One overlooked radius can increase tooling costs. Keep communication in writing, with revision numbers and signed drawings, so every change remains traceable.
Evaluate China’s Metal Stamping Capabilities and Processes
How to Find the Best Metal Stamping Parts in China?
Evaluate China’s Metal Stamping Capabilities and Processes
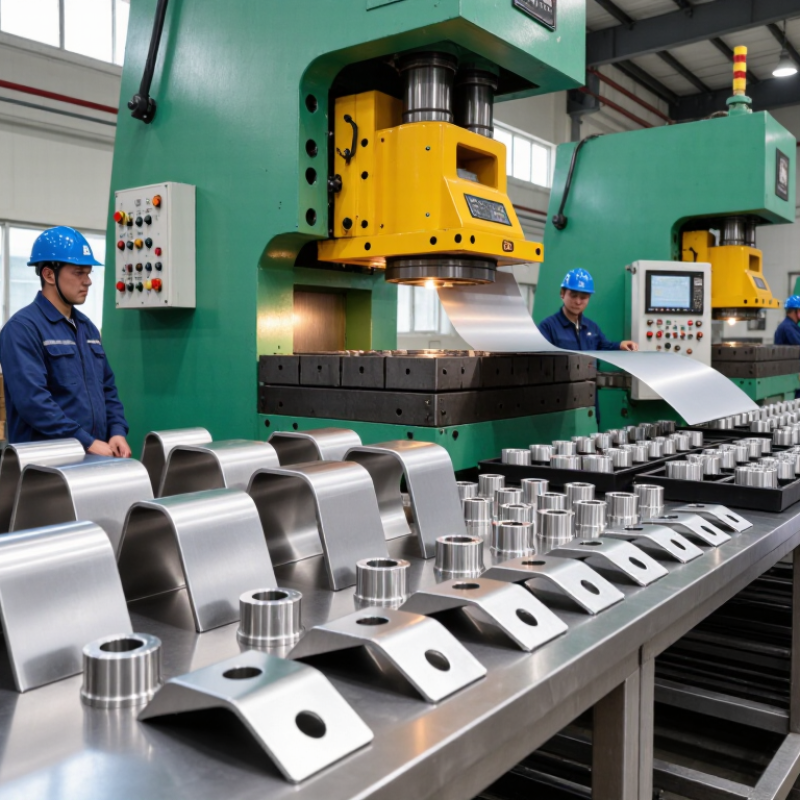
China’s metal stamping sector covers progressive, deep-drawing, and four-slide operations. Each process suits different shapes, volumes, and material thicknesses. Ask the supplier to explain why a specific method fits your drawing. A capable engineer should discuss blank size, press tonnage, die life, and springback. Vague promises are warning signs.
Review the factory’s equipment directly. Check press capacity, feeding accuracy, die maintenance, and in-process inspection. For stainless steel, aluminum, or carbon steel, confirm the tested grades and thickness ranges. Request sample dimensional reports, not only attractive photographs. Critical features may include hole position, bend angle, burr height, and flatness. Keep tolerances realistic. Very tight tolerances can increase tooling costs without improving function.
Tooling quality deserves careful attention. Ask how dies are designed, trialed, repaired, and stored. A serious supplier can provide trial records and explain corrective actions. I have seen excellent first samples fail after several production runs because die wear was overlooked. That mistake is expensive. Check whether operators use gauges, coordinate measuring equipment, or optical inspection for critical dimensions. Traceable material certificates and batch records also improve reliability.
Communication matters. Send a complete drawing, surface-finish requirement, annual volume, and packaging specification. Then compare technical responses, not just unit prices. A lower quote may exclude tooling maintenance or secondary operations. Ask for a small pilot run before full production. It may reveal feeding problems, edge cracks, or inconsistent forming that a spreadsheet cannot show.
Verify Supplier Quality, Certifications, and Production Equipment
Finding reliable metal stamping parts in China starts with checking how a supplier controls quality, not how polished its website looks. Ask for process flow charts, inspection plans, and recent production records. Quality should be visible. Request sample reports showing dimensions, material grade, surface condition, and sampling methods. Compare these records with your drawings and tolerance requirements. Promises are not proof.
Certifications can support a supplier’s credibility, but they require verification. Check the certificate number, issuing organization, validity period, factory address, and approved scope. The scope should cover manufacturing activities related to your parts. Ask whether the quality system applies to the actual production site. You can also request corrective action records from previous audits. A certificate alone cannot guarantee consistent output. I have seen documents that looked acceptable but did not match the operating facility.
Production equipment deserves equal attention. Confirm press capacity, stroke length, feed accuracy, die protection, and available forming processes. Ask how often presses and measuring tools are maintained or calibrated. During a factory visit, observe material storage, die identification, first-piece approval, and in-process inspections. Check whether operators record defects instead of hiding them. This detail matters. A capable supplier should explain how it handles burrs, cracks, springback, and dimensional drift. You may also discover that your original tolerance is unnecessarily strict. That conversation can reduce cost, but only after testing confirms performance.
How to Find the Best Metal Stamping Parts in China? - Verify Supplier Quality, Certifications, and Production Equipment
Use the following criteria to compare metal stamping suppliers. The figures are practical industry benchmarks and verification requirements, not claims about any specific company.
| Evaluation Dimension | What to Verify | Recommended Benchmark | Required Evidence | Risk Level if Missing | Suggested Evaluation Method |
|---|---|---|---|---|---|
| Quality Management System | Whether the supplier operates a documented and audited quality management system. | ISO 9001:2015 certification with a current validity period and a scope covering metal stamping or precision manufacturing. | Valid certificate, certification scope, issuing body, audit date, and certificate verification record. | High | Confirm the certificate directly through the issuing certification body and review recent corrective-action records. |
| Automotive Quality Capability | Process controls for automotive or other safety-critical applications. | IATF 16949 certification when the parts are intended for automotive production or comparable risk-sensitive applications. | Current certificate, applicable manufacturing scope, process-audit results, and customer-specific requirement records. | High | Check whether the certificate covers the actual production site and the relevant stamping process. |
| Environmental Management | Control of waste, chemicals, energy use, and environmental compliance. | ISO 14001:2015 is a useful benchmark for suppliers with plating, cleaning, welding, or high-volume production processes. | Valid certificate, environmental permits where applicable, waste-disposal records, and chemical-management procedures. | Medium | Review the certificate scope and request evidence that outsourced surface treatment is controlled. |
| Material Traceability | Ability to trace raw material from the approved mill or distributor through production and shipment. | Lot or heat-number traceability for each production batch, with material certificates available on request. | Mill test certificate, material grade, thickness, lot number, incoming inspection record, and production batch number. | High | Compare the material certificate with the purchase order, label, inspection report, and shipment documentation. |
| Press Capacity | Whether the equipment can safely produce the part using the required material, thickness, tooling, and draw depth. | Available press capacity should exceed the calculated forming requirement; common production ranges are approximately 25–800 metric tons. | Equipment list, press tonnage, bed size, stroke length, shut height, speed range, and maintenance records. | High | Match the part drawing and forming calculations against the press specification rather than relying on tonnage alone. |
| Press Type and Automation | Suitability of mechanical, servo, hydraulic, progressive, transfer, or four-slide equipment for the part geometry. | Progressive or transfer presses for high-volume complex parts; servo or hydraulic presses where forming control is important. | Machine model category, feeder type, line layout, automation photographs or video, and production cycle data. | Medium | Request a sample run or process-flow review using a tool design similar to the target part. |
| Dimensional Inspection | Capability to measure critical dimensions, profiles, flatness, hole locations, and form features. | Calibrated calipers, micrometers, height gauges, optical measurement, and CMM access when the drawing requires complex 3D inspection. | Equipment calibration certificates, inspection plan, measurement-system records, and sample dimensional report. | High | Check whether measurement resolution and accuracy are appropriate for the drawing tolerance. |
| Typical Dimensional Tolerance | Ability to hold the tolerances specified on the engineering drawing. | For standard stamped features, approximately ±0.05 to ±0.25 mm may be achievable depending on material, geometry, tooling, and process stability. | Capability study, first-article inspection report, control plan, and measurement data from multiple parts. | High | Use a first-article sample and request process-capability data for critical dimensions. |
| Process Capability | Statistical control of critical characteristics during mass production. | For critical dimensions, a common target is Cpk ≥ 1.33; stricter programs may require higher values. | Control charts, capability study, inspection frequency, reaction plan, and nonconformance records. | High | Review the sample size, measurement method, data distribution, and whether the study represents normal production. |
| Tooling and Die Maintenance | Control of progressive dies, compound dies, transfer dies, and replacement components. | Documented preventive-maintenance schedule, spare-part strategy, die-life tracking, and change-control procedure. | Tooling drawings, maintenance log, die inspection checklist, repair history, and ownership terms. | High | Inspect the toolroom and confirm who owns, stores, maintains, and modifies the tooling. |
| Surface and Corrosion Protection | Control of deburring, cleaning, coating, plating, passivation, or oiling requirements. | Process parameters and acceptance criteria must match the drawing or purchase specification; salt-spray requirements should be defined by the application. | Coating or plating certificate, thickness report, appearance standard, salt-spray report when required, and approved subcontractor list. | High | Verify both the stamping supplier and any outsourced finishing process through documented inspection results. |
| Regulatory Compliance | Restrictions on hazardous substances and chemical content for the destination market. | Declaration or test evidence for RoHS and REACH compliance when required by the product application or market. | Supplier declaration, material declaration, laboratory test report, and controlled chemical-substance list. | Medium | Confirm that evidence applies to the exact material, coating, plating, and supplied part number. |
| Production Capacity | Ability to meet forecast volume without excessive overtime, subcontracting, or unstable lead times. | Capacity plan should show available press hours, tooling capacity, staffing, maintenance downtime, and contingency resources. | Monthly capacity report, utilization data, production schedule, bottleneck analysis, and backup-process plan. | Medium | Compare forecast demand with verified machine hours and actual output from a comparable part. |
| First Article and Production Approval | Formal approval before regular production begins. | First-article inspection covering all drawing dimensions, materials, appearance criteria, and functional requirements. | Signed first-article report, approved samples, control plan, process-flow chart, and packaging specification. | Required | Make production approval conditional on passing the agreed sample and documentation review. |
| Supplier Audit Readiness | Transparency of the factory, records, subcontractors, and corrective-action system. | Willingness to support an on-site or remote audit and close nonconformities with documented root-cause analysis. | Audit checklist, corrective-action report, evidence of closure, organization chart, and approved subcontractor register. | High | Use a risk-based audit covering quality, equipment, tooling, materials, traceability, and final inspection. |
Compare Quotes, Tooling Costs, Lead Times, and Minimum Orders
Finding the best metal stamping parts in China starts with a comparable request for quotation. Send identical drawings, material grades, thicknesses, tolerances, surface requirements, packaging details, and annual volumes. Otherwise, a low quote may simply omit inspection or secondary operations. Ask each supplier to separate piece price, tooling cost, sampling fees, packaging, and freight. Clear numbers matter.
Tooling deserves careful attention. A simple die may cost less, while a progressive die can support faster production and stable accuracy. Request the expected tool life, maintenance plan, repair charges, and ownership terms. Confirm whether tooling changes are included after design approval. Small details become expensive later.
We learned this after comparing two quotes that used different steel assumptions. The cheaper offer was not truly cheaper.
Lead time should be divided into engineering, tool fabrication, first samples, approval, and mass production. Ask for realistic dates, not only a total number. Verify production capacity during your required season. Minimum order quantities also affect cash flow and storage. A supplier accepting a small trial order may charge more per part, but this can reduce risk. Request sample inspection reports, material certificates, dimensional records, and photos of packed goods. Communication quality is evidence too. If answers remain vague, reconsider the quotation. Perfect planning is impossible, but transparent assumptions make problems easier to control.
Inspect Samples and Establish Reliable Quality Control Procedures
Finding the best metal stamping parts in China starts with inspecting physical samples, not relying on photographs. Request samples made with the intended material, thickness, tooling method, and surface finish. Measure critical dimensions with calibrated calipers, micrometers, and gauges. Check hole positions, edge conditions, flatness, burrs, and visible cracks.
Ask the supplier for material certificates and process records. Compare the sample with your approved drawing and tolerance requirements. Test fit matters. A part can pass a dimensional check yet fail during assembly. We once focused too heavily on outer appearance and missed a small spring-back issue. That mistake changed our inspection checklist.
Create a written quality control procedure before mass production begins. Define inspection points for incoming material, first-piece approval, in-process checks, and final packing. Set clear sampling levels and specify what happens when a defect appears. Keep inspection photos, measurement data, lot numbers, and corrective-action reports. These records make supplier discussions more factual and traceable.
Use an independent inspection when the part is safety-critical or technically complex. Confirm that inspectors understand your drawings and measurement methods. Production speed should never replace process stability. However, excessive checks can slow delivery without improving quality. Review the procedure after each production run, especially when defects repeat. A reliable supplier should accept reasonable audits, communicate problems early, and show evidence of corrective action. Trust grows through consistent records, not promises.
Article Source:
Let's Work Together
The most innovative products come from the most innovative people - and for over 55 years our team has been propelled by curiosity and a steadfast dedication to inventing and creating the best foam formulations for our customers.