2026 Top Smart Paging Machine Manufacturers and Suppliers

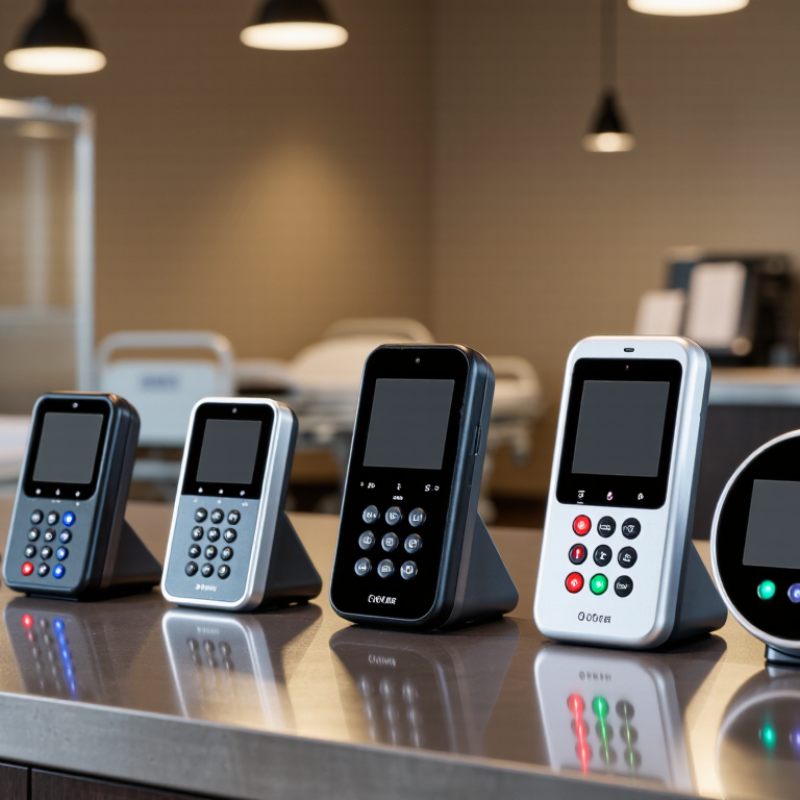
Smart Paging Machine suppliers now serve restaurants, hospitals, hotels, and busy service counters. Buyers want more than a flashing receiver. They need reliable signal coverage, clear alerts, durable hardware, and simple day-to-day operation.

Market reports offer useful context, though they do not isolate Smart Paging Machine sales. Fortune Business Insights estimated the global nurse call systems market at about USD 2.4 billion in 2023, with further growth projected through 2032. That figure describes an adjacent healthcare category, not the paging-machine market itself. The distinction matters. A hospital call system and a restaurant guest pager solve related, but different, problems.

Manufacturing quality expert W. Edwards Deming said, “It is not necessary to change. Survival is not mandatory.” His warning suits equipment selection: low upfront cost means little if receivers fail during peak service. Still, no single specification tells the whole story. A supplier’s range, battery performance, warranty terms, and support response deserve close review. Ask how the system performs behind a kitchen wall, across a hotel lobby, or after months of daily charging. Then compare answers, not just catalog claims. This 2026 guide examines manufacturers and suppliers through practical buying criteria, product fit, and available evidence. Some details remain hard to compare across vendors. That is a reason to verify them, not to assume.
2026 Top Smart Paging Machine Manufacturers and Suppliers

Smart Paging Machines: Core Functions, Feed Systems, and Product Types

Smart paging machines separate, count, and deliver sheets or flat products in a controlled sequence. Typical functions include page separation, batch counting, alignment, and automatic stopping when a sensor detects a misfeed. Some systems also stack completed sets or mark batches for downstream handling. Small gaps matter. A slightly curled sheet can trigger double-feeding, so operators should test with the actual paper weight, coating, and size.

Feed systems shape machine performance. Friction-feed designs use rollers or belts to pull sheets from a stack; they are practical for many standard papers, but surface wear can affect consistency. Vacuum-feed systems lift sheets with suction and may handle delicate or coated stock more gently. Hopper capacity, side guides, roller pressure, and sensor placement all influence reliable feeding. Paper is not uniform. Humidity and static can change how sheets separate, even during the same shift.

Product types range from compact desktop pagers for modest batches to production models with higher speeds and larger feeders. Integrated systems may combine paging with counting, collating, or conveyor delivery. When comparing suppliers, check supported material ranges, adjustment time, jam access, and available service documentation—not speed alone. Ask for a test using representative stock. One caveat: published capacity figures may assume ideal conditions, and real jobs rarely behave perfectly.

How Sensors, Servo Drives, and PLCs Coordinate High-Speed Page Separation

In a smart paging machine, high-speed page separation depends on sensors, servo drives, and PLCs working as one system. Optical sensors detect a sheet’s leading edge and report its position to the controller. Thickness or double-feed sensors can flag two pages moving together. The PLC uses these signals to adjust timing, while servo drives control rollers and separation belts with precise speed and position changes. A few milliseconds matter. If the feed roller advances too soon, pages may overlap or arrive skewed.

The PLC coordinates each handoff: sense the page, calculate the next movement, then command the servo. Feedback from encoders helps confirm that rollers actually reached their target speed. Operators still need to check paper curl, stack alignment, and sensor cleanliness; dusty lenses can make reliable detection less reliable. Even a well-tuned setup can drift. A practical test is to run different paper weights and inspect a sample of separated sheets for double feeds, edge damage, and spacing variation. Not every fault appears in the control screen. Adjustments should be gradual, because faster settings can expose weaknesses in the paper stack or mechanical alignment.

Performance Metrics: Throughput, Feed Accuracy, and OEE per ISO 22400

For 2026 smart paging machines, throughput is meaningful only when the test conditions are stated. Record good pages per minute, paper size, stock weight, and operating duration. A short run can hide jams that appear after a warm-up or a full shift. Feed accuracy should track correctly separated and positioned sheets against total sheets processed. Count skewed feeds, double-feeds, and missed pages separately. Small errors compound.

ISO 22400-2 provides a framework for manufacturing performance indicators, including OEE, built from availability, performance, and quality. Keep the calculation rules consistent across suppliers; otherwise, attractive scores may reflect different definitions. Deloitte’s 2024 Smart Manufacturing survey found that 86% of surveyed manufacturing executives viewed smart manufacturing as a likely competitiveness driver over the following five years. That is not a paging-machine benchmark, but it underlines why comparable, traceable data matter. Ask suppliers for shift-level logs, not just a peak-speed demonstration. A clean dashboard can still mislead.

For a practical comparison, request the same paper stock, run length, and fault-counting method from each supplier. Check whether OEE excludes planned changeovers, and whether rejected or manually corrected pages count as defects. These details are easy to overlook—and worth challenging.

Safety and Compliance: Machinery Controls Under ISO 13849-1, PL a–e

A paging machine may look simple: a feeder, a conveyor, and a stack of trays. Yet a hand reaching into a jam can expose a serious control-system weakness. ISO 13849-1:2023 helps designers assess safety-related parts of control systems and assign a required Performance Level, or PLr, from a to e. The required level comes from risk assessment; it is not a general safety grade for the whole machine. A guard interlock, emergency stop, and jam-clearing function may each need separate consideration. Small details matter.

For a real installation, engineers should check the complete safety function: sensor, logic, wiring, and final switching element. ISO 13849-1 evaluates factors including architecture, component reliability, diagnostic coverage, and common-cause failure. A door switch that detects access is not enough if a contactor can weld shut or the machine restarts unexpectedly. Eurostat’s 2022 workplace-accident statistics recorded 3.286 million non-fatal accidents in the EU involving at least four days away from work. That figure spans many industries, but it reinforces why routine tasks deserve careful review. Validate the achieved PL against the required PLr, test fault responses, and document results. A checklist helps, but it cannot replace testing on the actual machine.

2026 Top Smart Paging Machine Manufacturers and Suppliers - Safety and Compliance: Machinery Controls Under ISO 13849-1, PL a–e
Safety Function / Evaluation Area Typical Paging-Machine Application Potential Hazard Illustrative PLr Range Supplier Evidence and Verification Points
Guard-door interlocking Access doors around the paging head, conveyor, or other hazardous moving parts Access to moving components while hazardous motion is present c–e, risk-assessment dependent Request the safety-function specification, interlock and guard details, stopping-time assessment, and validation records. Confirm that guard locking is considered if a person could reach the hazard before motion stops.
Emergency-stop function Emergency-stop devices at operator and accessible work positions Failure to stop hazardous movement promptly in an emergency c–d, risk-assessment dependent Check device locations, reset behavior, stopping behavior, and test records. An emergency stop is a supplementary protective measure; it does not replace guarding or other risk-reduction measures.
Unexpected-start prevention Restart after a guard is closed, a fault is cleared, or power is restored Unexpected movement that could strike, trap, or entangle a person c–e, risk-assessment dependent Verify that a deliberate start command is required where appropriate and that reset does not itself initiate hazardous motion. Review restart behavior under normal and fault conditions.
Safe access for jam clearing Clearing misplaced labels, media, or product from the paging path Contact with moving rollers, belts, or mechanisms during intervention c–e, risk-assessment dependent Review access procedures, isolation points, interlocked access, and any safe operating mode. Confirm that foreseeable jam-clearing tasks are included in the machine risk assessment.
Safety-related stop of conveyor or feed motion Stopping product transport or feed motion when a protective device is activated Crushing, shearing, or drawing-in at moving interfaces c–e, risk-assessment dependent Ask which outputs and drive functions are stopped, how the stop is achieved, and how the complete safety-related control system was validated. Check that residual motion is considered.
Presence-sensing protective device Light curtain or other presence-sensing device at an accessible loading or discharge area Access to a hazardous zone during automatic operation c–e, risk-assessment dependent Check protective-device suitability, positioning, resolution, response time, and the measured stopping time used to determine the safety distance. Confirm that bypassing is controlled and justified.
Safety-related fault detection Monitoring of safety inputs, outputs, and relevant wiring faults A fault remaining undetected and preventing the protective function from operating b–e, risk-assessment dependent Request circuit diagrams and validation documentation identifying the selected architecture, diagnostic measures, and fault assumptions. Review component data for the intended safety use.
Performance Level (PL) documentation Safety functions implemented by safety-related parts of the control system Insufficient reliability or performance of a safety function PL a (lowest) to PL e (highest) For each safety function, compare the achieved PL with its required PL (PLr). Look for documented calculations and validation; a component’s PL rating alone does not establish the PL of the complete safety function.
Validation and lifecycle records Design review, commissioning, modification, and periodic safety checks Safety performance not maintained after installation, adjustment, or repair Based on each safety function’s PLr Review validation results, test procedures, maintenance instructions, and change records. Confirm that any modifications trigger an appropriate review of the affected safety functions.
Important: The PLr examples above are indicative only, not fixed requirements for paging machines. ISO 13849-1 requires the required Performance Level to be determined for each safety function through risk assessment. The achieved PL depends on the complete design, including architecture, component reliability, diagnostic coverage, common-cause measures, and validation. This table is a supplier-evaluation aid, not a certification or compliance determination.

How to Compare 2026 Manufacturers by Integration, Service, and Validation Data

Comparing 2026 smart paging machine manufacturers starts with your production line, not a polished brochure. Map each handoff: feeder, printer, camera, reject station, and line controller. Ask suppliers to document interfaces, supported data formats, and alarm routing. Small gaps matter. An undocumented field can turn a short installation into hours of manual checks.

Service quality is easier to compare when response times, spare-part availability, and remote support limits are stated in writing. Ask who handles commissioning and operator training, and request a sample maintenance schedule. Then review validation evidence: test logs, acceptance criteria, and results across relevant materials and operating speeds. A single accuracy figure tells little without its test conditions.

Use the same sample jobs and questions with every supplier. Check whether records link each page to a timestamp, job identifier, and inspection result. Ask to see a live demonstration, including a misfeed or unreadable mark. The comparison will not be perfect; plant conditions vary, and one trial cannot represent every shift. If a data set seems unusually clean, ask what was excluded and why.

Let's Work Together

The most innovative products come from the most innovative people - and for over 55 years our team has been propelled by curiosity and a steadfast dedication to inventing and creating the best foam formulations for our customers.